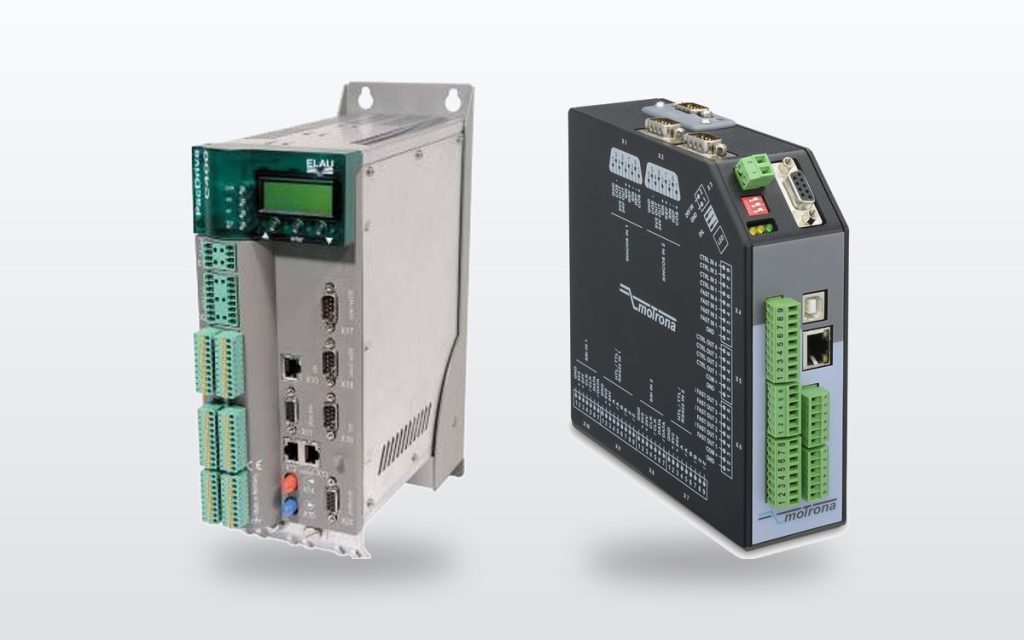
Short answer: use a PLC with motion function blocks — or intelligent drives — when axes move mostly independently at moderate dynamics. Use a dedicated motion controller, or a controller with an integrated high-performance motion engine, when several axes must stay tightly synchronised, when cycle rates are high, or when motion profiles change with every product.
What each option is good at
| Consideration | PLC with motion functions | Dedicated motion controller |
|---|---|---|
| Independent point-to-point moves | Well suited | Well suited |
| Electronic gearing and cams across many axes | Possible, platform-dependent | Core strength |
| Registration / print-mark correction | Limited on some platforms | Core strength |
| Motion update cycle | Tied to PLC task and network cycle | Typically short and deterministic |
| Maintenance familiarity | Usually high in plants | Requires specific skills |
| Hardware count | Lower | Additional controller |
Questions that decide it
- How many axes must be synchronised with each other? One master and one follower can often be handled by a synchronisation controller or intelligent drive. Six axes on cams around a virtual master is a motion-controller job.
- What is the cycle rate and required accuracy? Higher rates reduce the tolerance for jitter between the logic scan and motion updates.
- Do profiles change per product? Recipe-driven cam tables favour platforms with strong cam tooling.
- Who will maintain it? A solution the maintenance team can diagnose is worth more than a marginally faster one they cannot.
- What is standard in the plant or at the OEM? Standardisation reduces spares and training.
Hybrid architectures
Many machines use both: the PLC runs sequence, safety and line communication, while a motion controller or motion-capable drive handles the synchronised axes. The interface between them — which signals, which network, which side owns which state — should be designed explicitly.
If you are deciding for a specific machine, ask an NSPL engineer with the axis count, cycle rate and control platform.
Frequently asked questions
Can a PLC control servo motors?
Yes. Most current PLC platforms can command servo drives over a fieldbus using standardised motion function blocks. This works well for independent positioning axes and moderate synchronisation. Demanding multi-axis synchronisation is usually better served by a dedicated or integrated motion controller.