Products
Hover over or tap a product to see its key features.
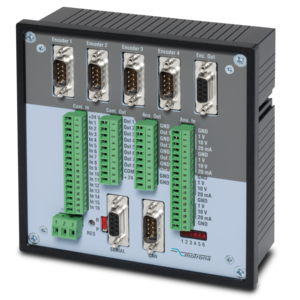
motrona MC700 – Universal Motion Controller, up to 4 Axes
Universal controller for up to four axes, used for synchronisation, index and print-mark control, rotary cross cutters, flying saws and label printing machines. Firmware for each application is loaded from the motrona application library.
- 4 incremental inputs (TTL/RS422) up to 400 kHz; 1 RS422 output
- 4 analogue outputs ±10 V; 4 analogue inputs; 16 inputs / 8 outputs
- RS232/RS485 and CANopen; 18–35 VDC supply
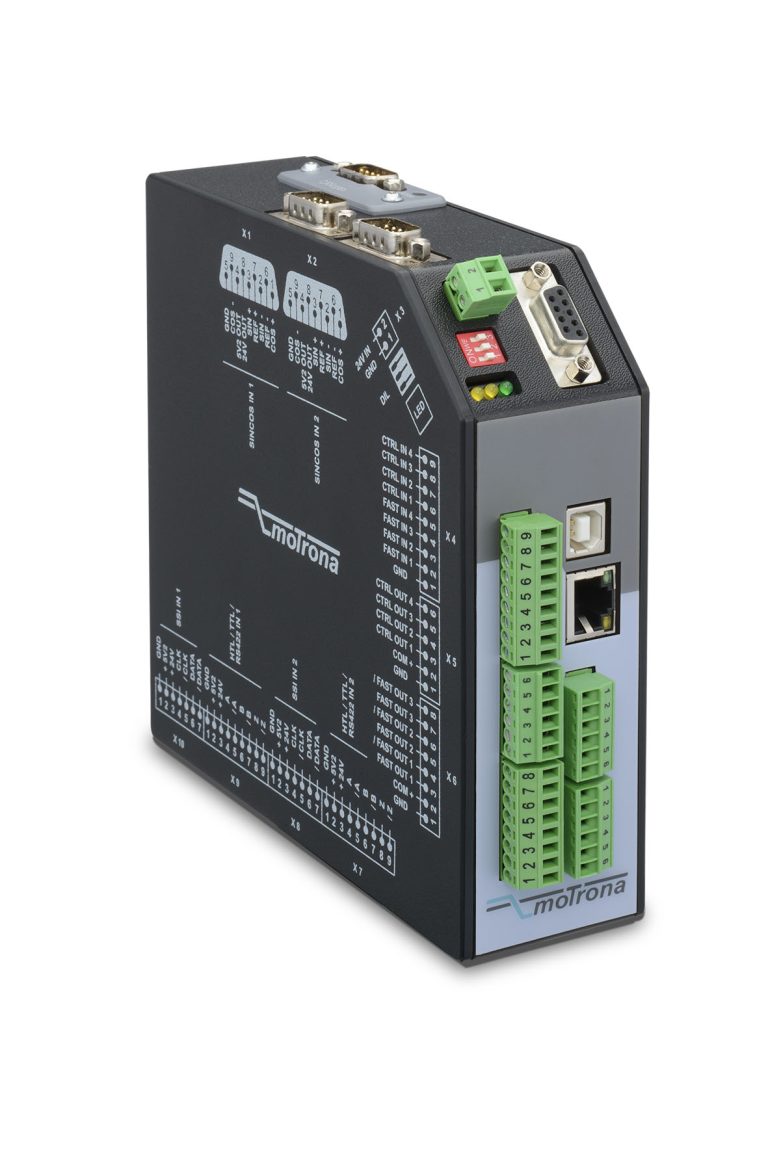
motrona MC800 – High-Performance 2-Axis Motion Controller
Powerful two-axis controller with high bandwidth and a flexible bus architecture. Accepts incremental, HTL and sine/cosine encoders, and runs optimised firmware for synchronisation (BY801), flying processing (FS801) or rotary processing (CT803).
- Inputs: RS422/HTL incremental, 1 Vpp sin/cos; 4 fast digital inputs
- 2 x 14-bit analogue inputs and ±10 V analogue outputs
- Ethernet, CANopen, Modbus RTU, RS232/RS485; optional EtherCAT, PROFINET, PROFIBUS
motrona MC800 – 2-Axis Motion Controller (Alternative View)
Alternative view of the MC800 DIN-rail motion controller. Its integrated tandem drive function splits power between two independent drives to master the acceleration of heavy loads in cutting lines, saws and mobile equipment.
- Snap-on 35 mm DIN-rail module
- Integrated tandem drive control for heavy loads
- USB and Ethernet front ports for set-up and communication
Applications in motion
Animated examples of how these controllers are used on real machines.
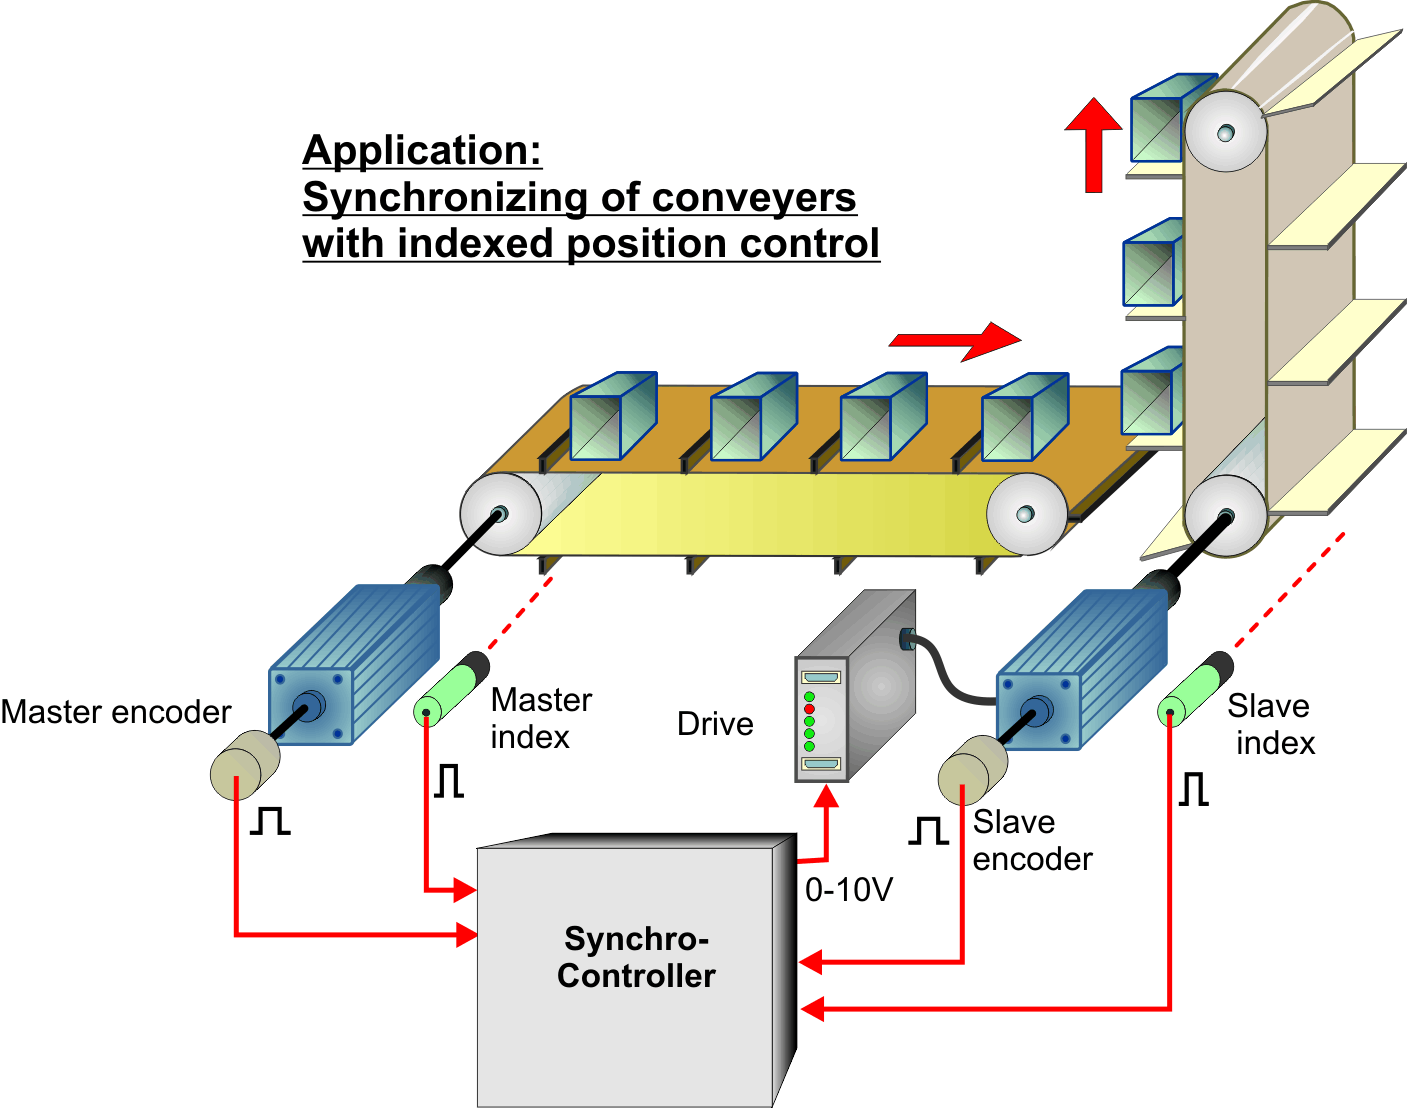
Application: Conveyor Synchronisation with Indexed Position Control
A motrona synchro-controller reads master and slave encoders plus index marks from both conveyors and sends a 0–10 V correction to the slave drive. Products are handed over in exact position, for example from a belt onto a vertical shelf conveyor.
- Master/slave encoder and index sensor inputs
- 0–10 V speed correction to the slave drive
- Position-accurate product transfer between conveyors
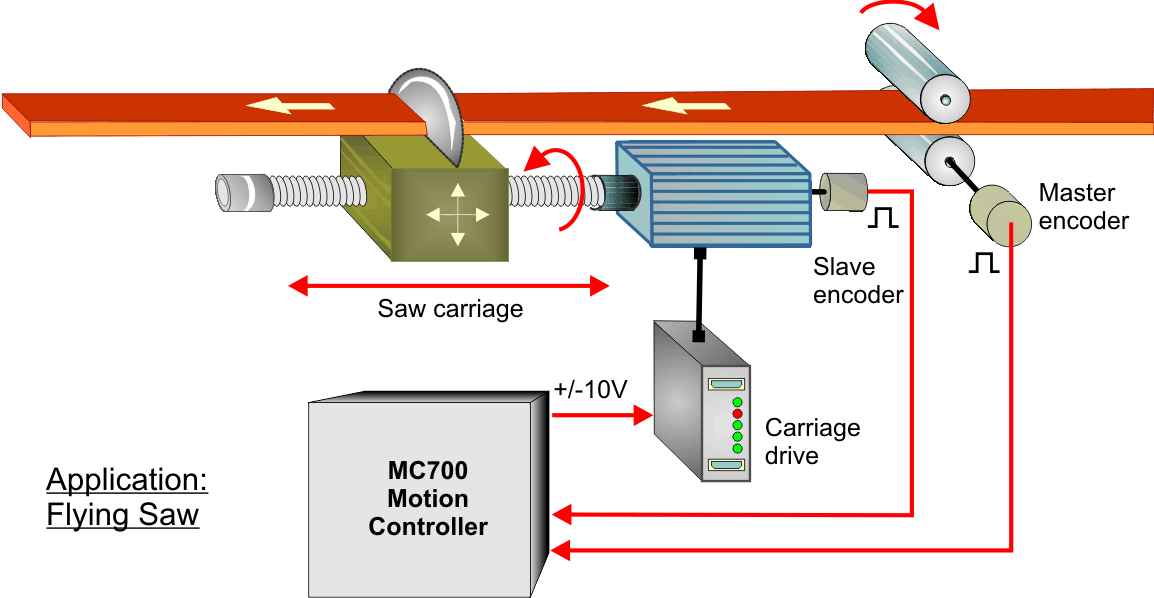
Application: Flying Saw
The MC700 motion controller accelerates the saw carriage to match line speed, holds it synchronous during the cut and returns it for the next length. Master and slave encoders feed the controller, which drives the carriage via ±10 V.
- Cut-to-length on the fly without stopping the line
- Master (line) and slave (carriage) encoder feedback
- ±10 V speed reference to the carriage drive
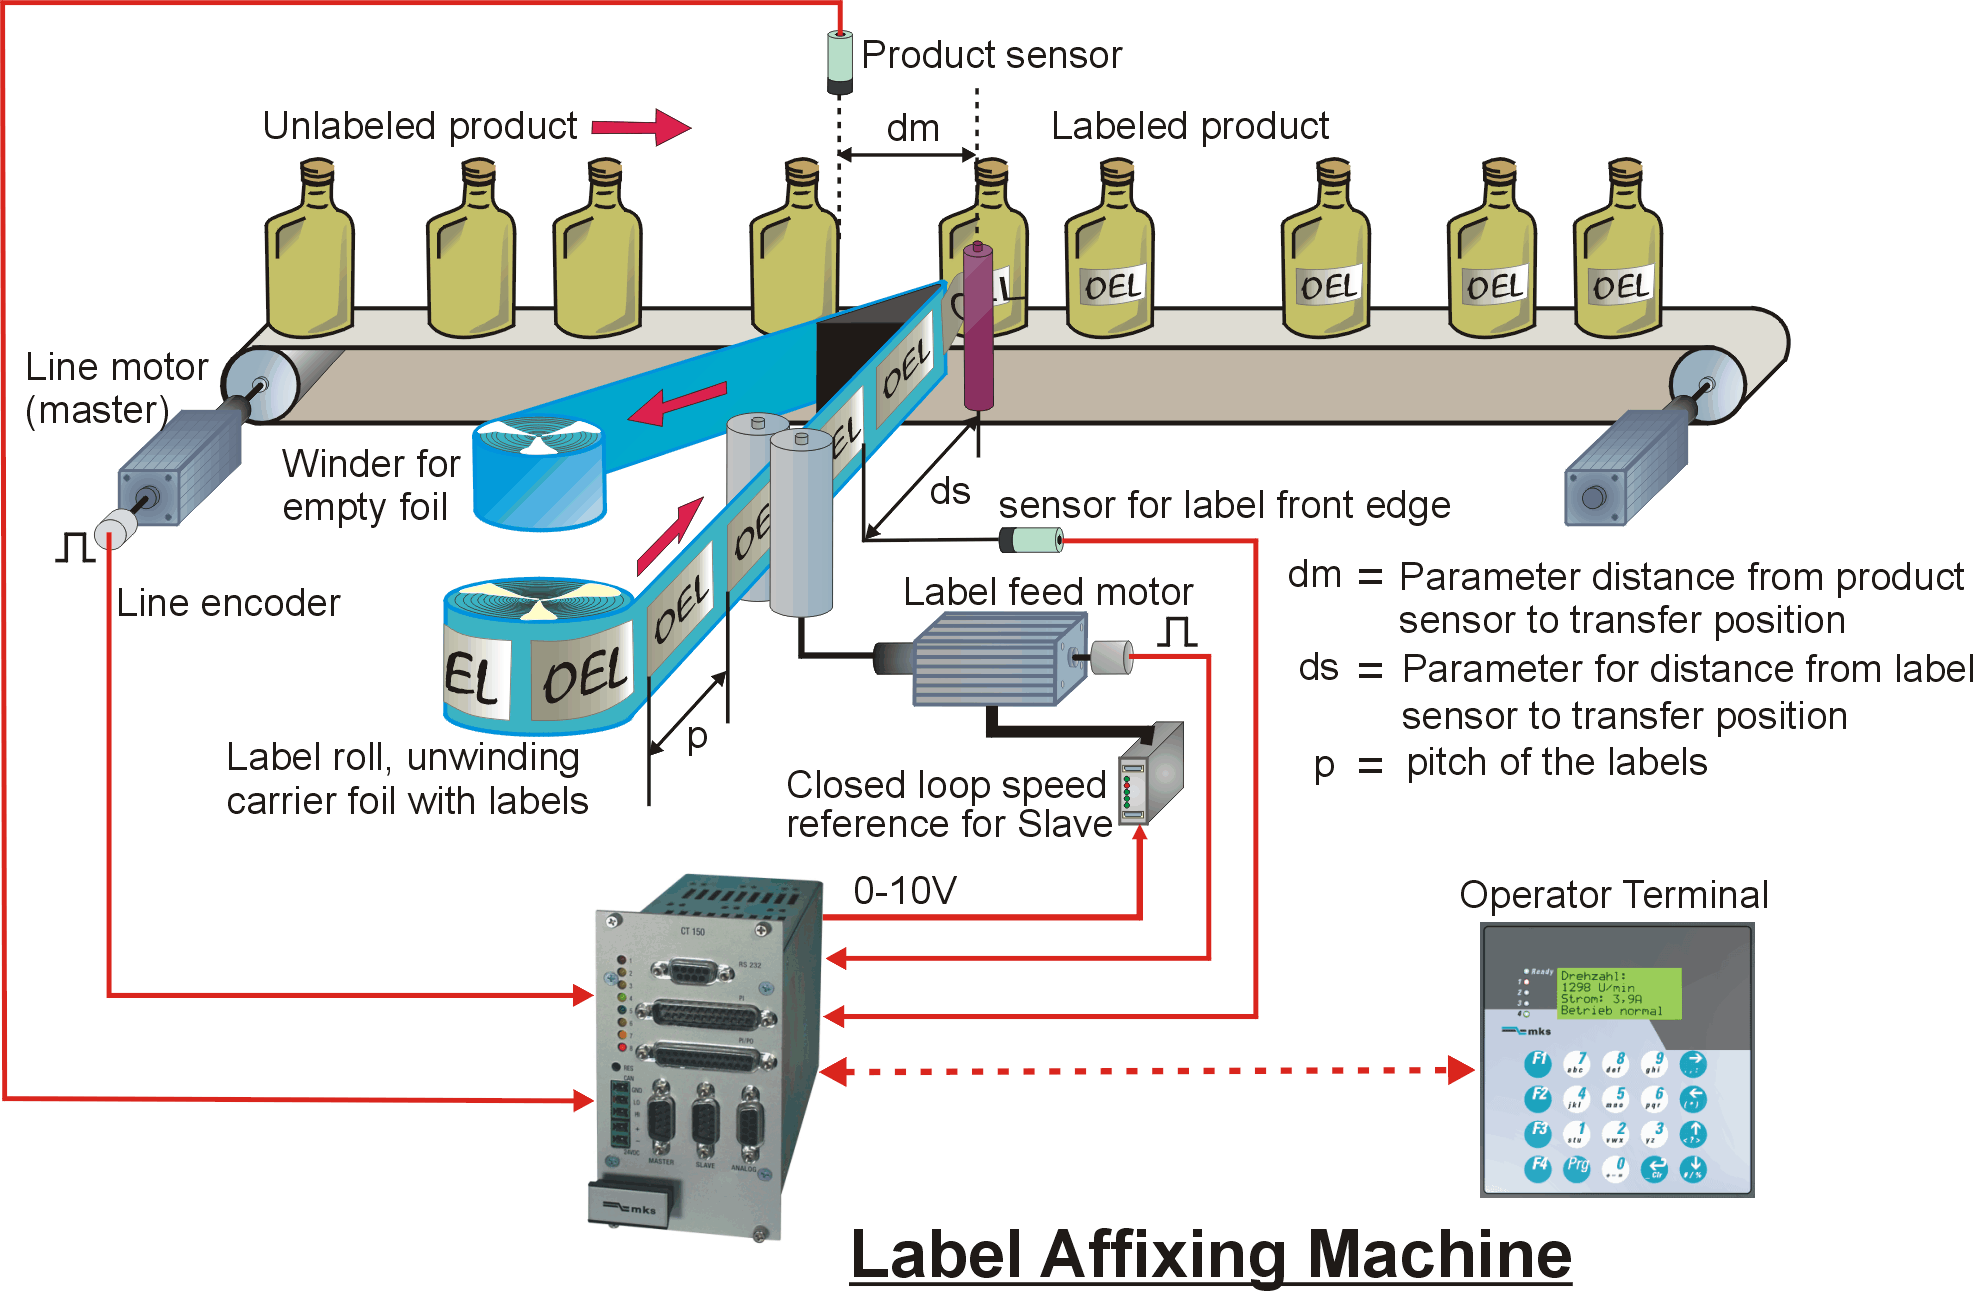
Application: Label Affixing Machine
A motrona controller synchronises the label feed motor with the line conveyor. Product and label-edge sensors, together with programmable distances (dm, ds) and label pitch, place every label precisely on each product, with set-up via operator terminal.
- Line encoder as master, label feed motor as slave
- Product and label-front-edge sensors for exact placement
- Closed-loop 0–10 V speed reference; operator terminal set-up
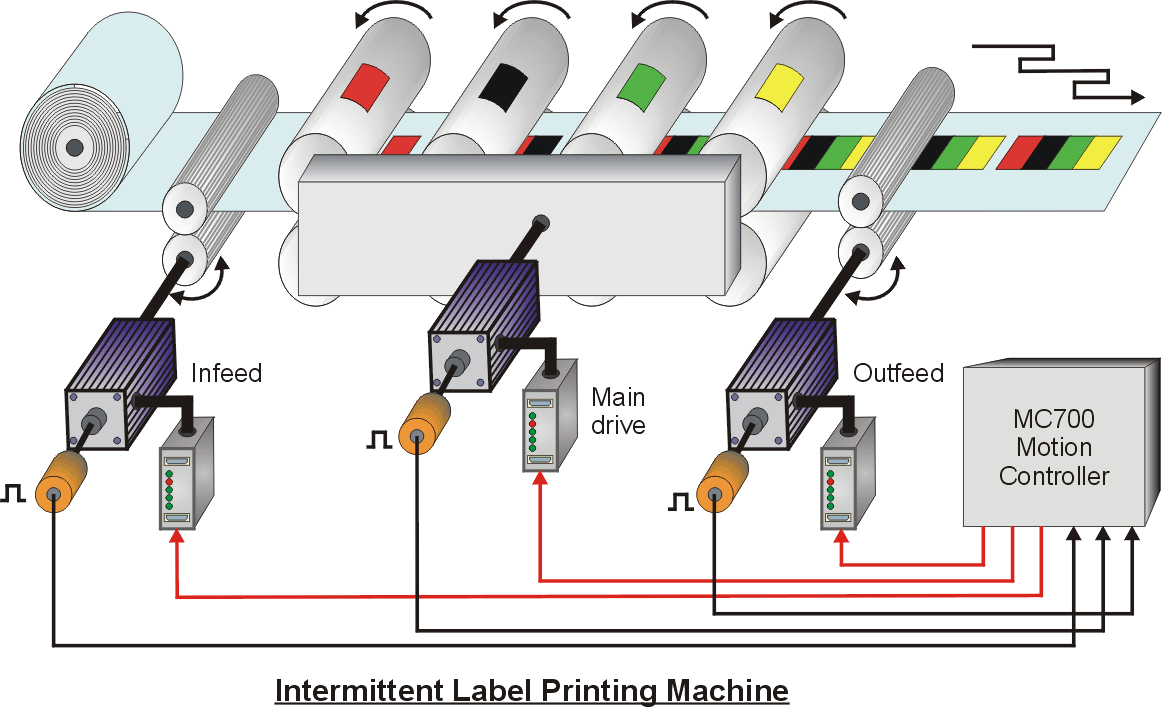
Application: Intermittent Label Printing Machine
The MC700 motion controller coordinates infeed, main drive and outfeed of an intermittent label printing machine, so the web stops, prints in register and restarts with precise positioning at every cycle.
- Three-axis coordination: infeed, main drive, outfeed
- Encoder feedback from each axis
- Accurate print register in intermittent operation
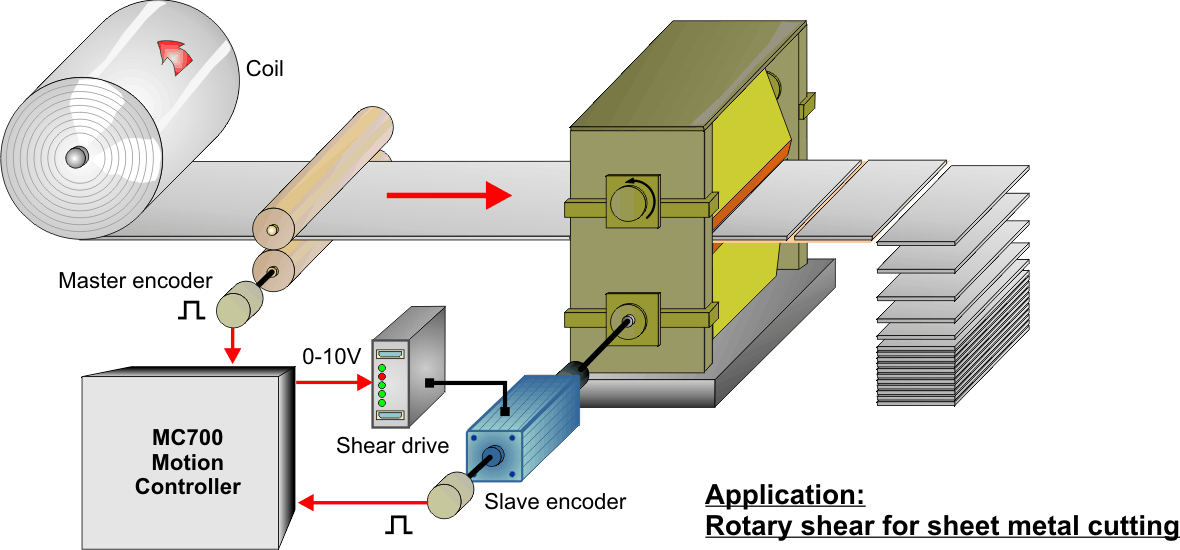
Application: Rotary Shear for Sheet-Metal Cutting
The MC700 motion controller synchronises the rotary shear with the sheet coming off the coil, using master and slave encoders and a 0–10 V reference to the shear drive. Sheets are cut accurately to length without stopping the line.
- Master encoder on infeed rolls, slave encoder on shear
- 0–10 V speed reference to the shear drive
- Continuous cut-to-length of coil material
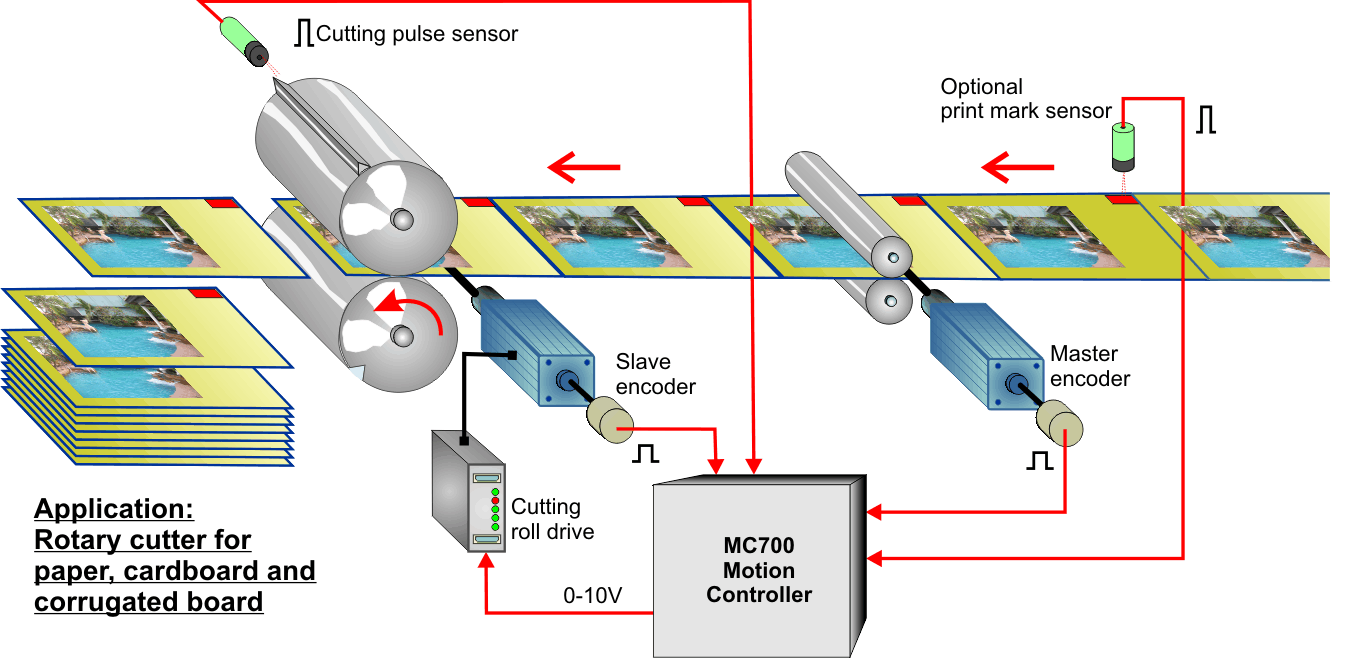
Application: Rotary Cutter for Paper, Cardboard & Corrugated Board
The MC700 motion controller drives the cutting roll in sync with the web, using master and slave encoders and a cutting-pulse sensor. An optional print-mark sensor corrects the cut position, so printed sheets are cut in register.
- Cutting-pulse sensor and optional print-mark correction
- Master/slave encoder synchronisation
- 0–10 V reference to the cutting roll drive
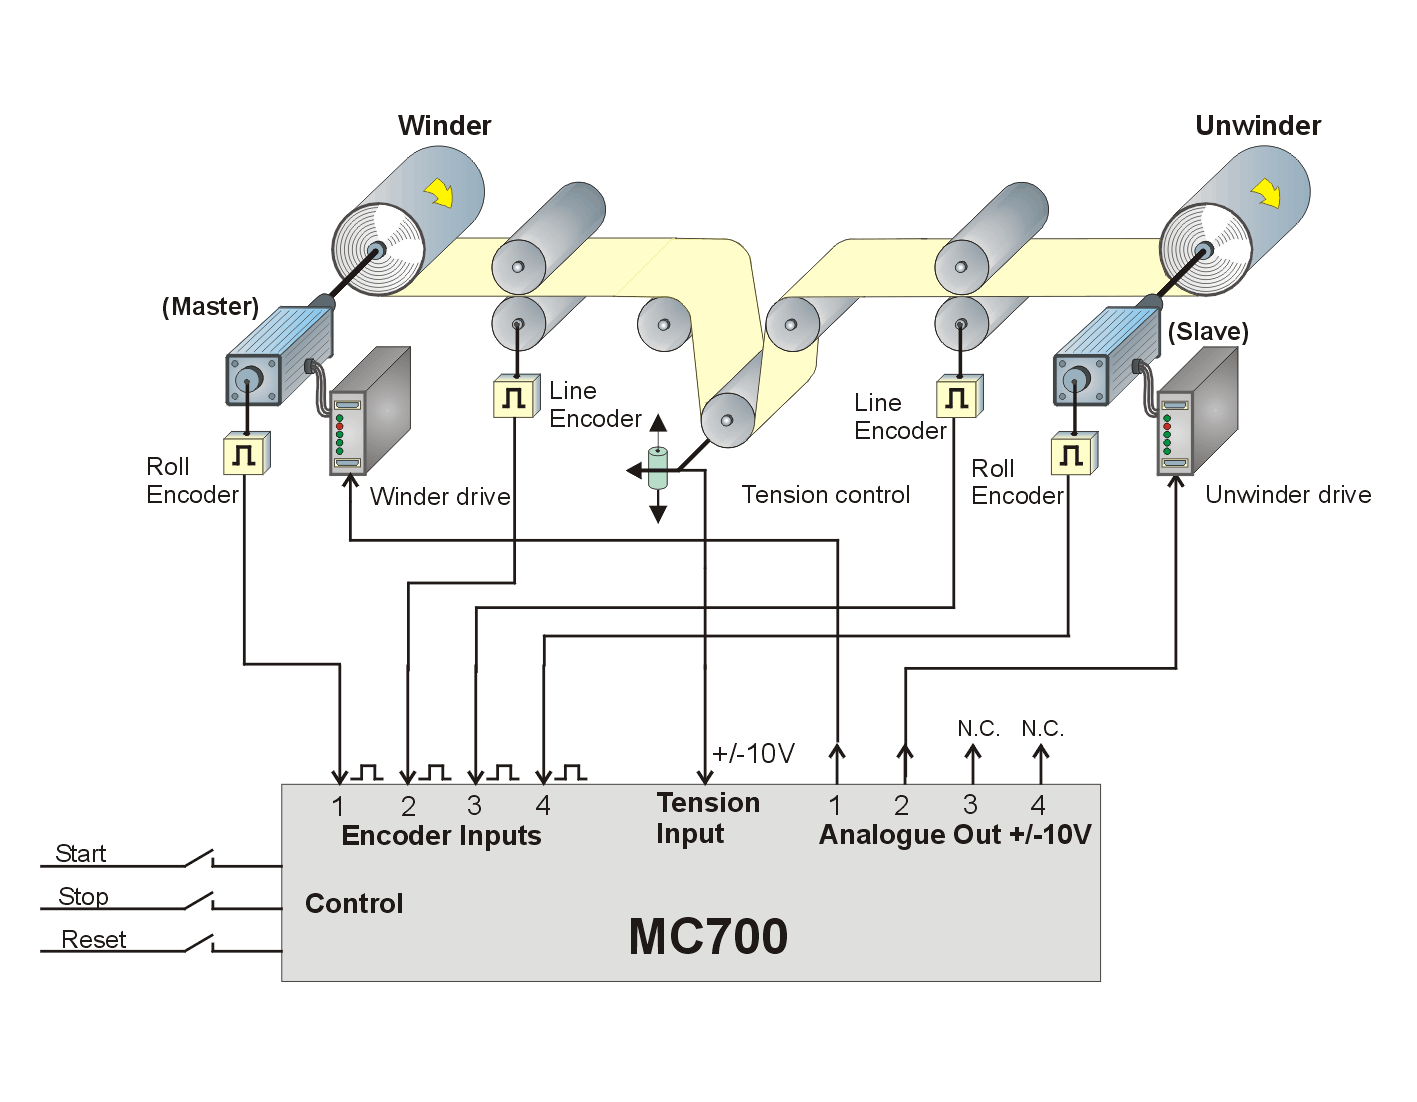
Application: Winder / Unwinder Tension Control
The MC700 coordinates winder and unwinder drives using roll and line encoders plus a tension input. Its ±10 V analogue outputs keep web tension constant as roll diameters change, with simple start, stop and reset control.
- 4 encoder inputs: roll and line encoders on both sides
- Tension input (±10 V) for closed-loop control
- ±10 V outputs to winder and unwinder drives
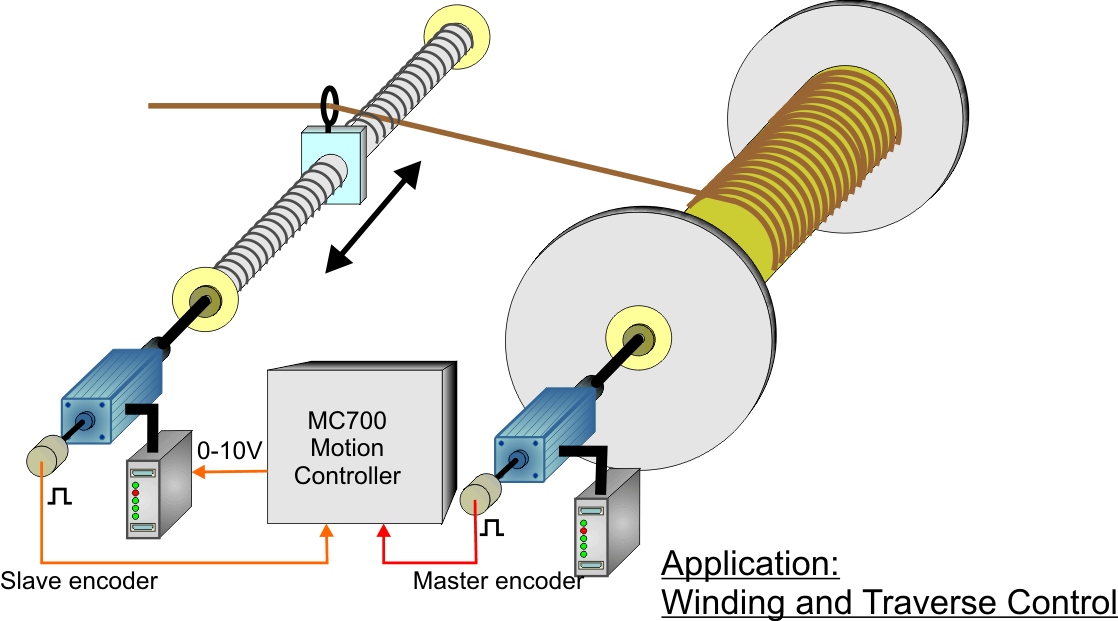
Application: Winding and Traverse Control
The MC700 motion controller links the traverse axis to the winding spindle via master and slave encoders, laying wire, cable or yarn evenly across the spool for perfectly formed coils.
- Master encoder on spindle, slave encoder on traverse
- 0–10 V reference to the traverse drive
- Even, layer-accurate winding of wire, cable and yarn
Need a specific model, a replacement for an installed unit or help choosing? Send the model or part number or ask an engineer.
Supplied and supported by NSPL as a principal partner of Motrona.